SiC Coated Graphite Manufacturer: Advanced Coating Solutions for Semiconductor and Solar Industries
2026-11-02
In the high-stakes world of semiconductor and solar manufacturing, every component must withstand extreme conditions without compromising purity or performance. SiC coated graphite has emerged as a game-changing material, offering exceptional thermal stability, chemical resistance, and durability. But not all coatings are created equal. Semicorex has refined the art of silicon carbide coating to deliver advanced solutions that push the boundaries of what's possible in wafer processing and photovoltaic production. This blog explores why SiC coated graphite is indispensable, the engineering challenges behind perfect adhesion, and how Semicorex is redefining reliability for modern fabs and solar lines. Whether you're battling particle contamination or seeking longer component lifetimes, the insights ahead will change how you evaluate coating suppliers.
Coating Chemistry That Withstands Extreme Thermal Cycling
Thermal cycling punishes ordinary coatings through repeated expansion and contraction. The real culprit is rarely the temperature itself but the mismatch in coefficient of thermal expansion between the substrate and the film. A coating that survives must either flex with the substrate or absorb the strain without cracking. Chemists address this by building polymer backbones with alternating rigid and flexible segments. Siloxane linkages, for example, provide low rotational energy barriers, allowing chains to relax before stress concentrates. Combined with aromatic rings that raise glass transition temperatures, this balance keeps the network dimensionally stable at high heat yet pliable enough at cryogenic conditions.
Beyond backbone choice, crosslink density determines how a coating handles thermal shock. Too many crosslinks create a brittle, glass-like film that shatters after a few cycles; too few leave it soft and prone to flow. Modern formulations move toward hybrid organic-inorganic structures where ceramic-like nodes are tethered by organic spacers. These nodes act as anchors, preventing large-scale chain movement while the spacers absorb local deformation. Adding nano-scale plate-like fillers further helps by deflecting crack propagation, forcing any micro-fractures to take a tortuous path instead of splitting straight through the film.
The true test comes from rapid cycling between liquid nitrogen and a hot plate, often repeated thousands of times. Past generations of coatings would begin showing edge lifting or micro-crazing within the first hundred cycles. Newer chemistries, based on dual-cure mechanisms that first build a dense protective surface and then a tougher, more elastic underlayer, routinely exceed several thousand cycles without visible damage. This layered approach lets the surface resist abrasion and chemical attack while the base layer manages the mechanical stress, so the entire system keeps its adhesion and barrier properties through extremes that would destroy conventional single-layer films.
Graphite Grades Selected for Semiconductor-Grade Purity
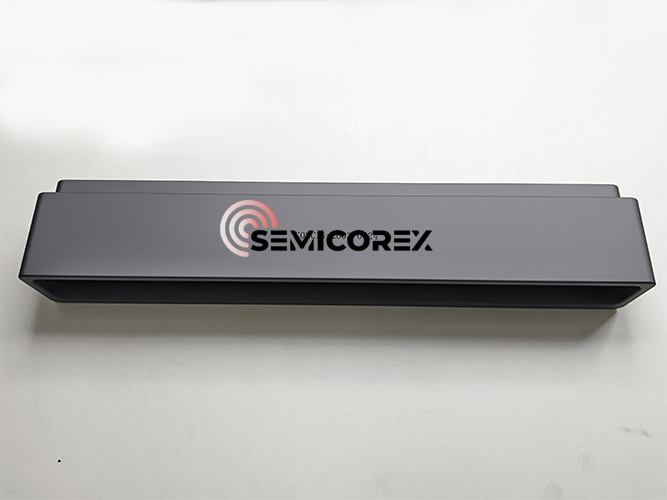
Producing graphite for semiconductor tooling starts with the raw coke and binder system, but the grade selection itself is what separates a chamber-ready material from a contaminated one. Fine-grained isostatic graphite with ash content below 5 ppm is the usual baseline, while demanding implant or etch applications lean on grades purified to sub-ppm levels. The difference shows up in trace metals—sodium, potassium, iron, copper—that can migrate into wafers even at parts-per-billion concentrations.
Purification routes matter. Halogen gas treatment at high temperature removes metallic impurities that acid washing misses, especially boron and vanadium. Some manufacturers blend multiple purification passes to get consistent low-ash performance across large billets. The chosen grade must also have uniform pore distribution and high thermal conductivity, because localized hot spots accelerate impurity release. Rather than simply choosing the "purest" label, process engineers often validate each lot against total ash, specific metal panels, and outgassing under vacuum.
For critical chamber parts like heaters, susceptors, and ion implant components, grades are often specified by both particle size and isotropy. Dense, fine-grain graphite with median particle size around 5-10 microns provides machinability and reduces particulate shedding. The semiconductor-grade designation is not a single standard; it is a set of material tolerances tied to the process step. A grade that works for a low-temperature etch electrode may fail in a high-temperature epitaxy environment due to different impurity volatility and thermal cycling demands.
Uniform SiC Layers for Repeatable Wafer Carrier Performance
A wafer carrier coated with silicon carbide only performs as well as the consistency of that coating. Thickness variations across the surface translate directly into uneven heat transfer during deposition or etch steps, which shows up as non-uniform film properties on the wafers themselves. By controlling the SiC deposition process tightly—particularly the gas flow and temperature ramp during CVD—the layer stays within a narrow tolerance, edge to edge. That repeatability in the physical layer is what keeps process engineers from chasing wafer-to-wafer drift.
Uniformity also affects how the carrier sheds particles and resists wear over hundreds of thermal cycles. A smooth, even SiC surface minimizes micro-cracks and stress points where flaking can begin. When the layer thickness is consistent, the carrier expands and contracts more predictably during heating and cooling, so the coating does not delaminate early. Fewer particles and longer intervals between carrier replacements mean less tool downtime and more stable baseline performance.
Perhaps the most underappreciated benefit is the reduction in process recipe adjustments after a carrier change. Operators know that a new carrier with a slightly different SiC thickness profile can shift temperature readings by a few degrees, forcing re-qualification runs. Uniform layers from one carrier to the next remove that variable. In production fabs, that translates to faster recovery after maintenance and a cleaner match between qualification wafers and actual product runs.
Tailoring Coating Thickness to Each Furnace Profile
Furnace profiles differ widely from one installation to the next, and a coating thickness that holds up in one thermal environment often fails in another. Rather than applying a standard layer, it makes more sense to map the hottest and coldest zones along the load path, then vary the deposition rate accordingly. For example, in a continuous furnace with a sharp temperature ramp near the entrance, a slightly thinner coat on the first few feet of the workpiece allows the substrate to expand without cracking the layer, while the soak zone receives a heavier build to resist prolonged oxidation.
The adjustment itself can be carried out through several process levers. Spray nozzle distance, line speed, and coating viscosity each influence the final dry film thickness, and these can be tuned zone by zone once the thermal profile is known. On a walking beam furnace, operators often raise the coating weight over areas that align with the burner impingement points, since those spots experience both higher heat flux and more mechanical abrasion. Conversely, reducing the coat near the discharge end can prevent spalling when parts cool unevenly.
Verification should follow the same zone-based logic rather than relying on a single thickness reading. Thickness sensors placed at three or four locations along the furnace length, combined with periodic coupon tests, help confirm that the applied profile matches the actual heat distribution. This practice not only stretches the coating material further but also lowers the frequency of unplanned shutdowns, because weak spots are addressed before they become failure points.
Solar Manufacturing Demands a Different Kind of Durability
When people think of durability in manufacturing, they often picture heavy steel frames, thick welds, and coatings that resist rust after years of rain and salt spray. Solar panel production throws most of that intuition out the window. The real enemy here is not corrosion from weather but the slow, invisible degradation caused by thermal cycling, humidity penetration, and relentless UV exposure at the material level. A solar cell that loses a fraction of a percent in efficiency each year might still look fine from the outside, yet over two decades that adds up to a panel that simply can't pay for itself.
The challenge is that solar modules are laminated sandwiches of glass, polymer encapsulants, silicon cells, and backsheet films, each with its own expansion rate and chemical sensitivities. Traditional industrial equipment is built to survive mechanical stress; solar materials must survive chemical and photonic stress. That means durability tests have to simulate decades of sun, cloud, rain, and temperature swings in weeks, often using accelerated weathering chambers that cycle from minus forty to plus eighty-five degrees Celsius while blasting UV light and condensing humidity. Only materials that survive this gauntlet without delaminating, yellowing, or losing adhesion are worth putting on a roof.
This shifts the entire manufacturing philosophy. Instead of asking how thick a frame should be, engineers ask how stable an encapsulant's cross-linking stays after a thousand damp-heat cycles. Instead of coating metal with paint, they deposit transparent conductive oxides that must not migrate under an electric field. Durability in solar manufacturing is not about brute strength; it's about molecular patience. A module that can sit in a desert for thirty years and still produce eighty percent of its original power is a triumph of chemistry and process control, not just physics and heavy machining.
Solving Complex Component Geometries Beyond Standard Shapes
Most off-the-shelf components work fine until a design calls for a load path that doesn’t follow straight lines or a flange that has to twist around an existing assembly. At that point, standard extruded profiles, turned cylinders, and flat plates stop being useful. The real challenge isn’t just making a weird shape—it’s holding tolerances on surfaces that can’t be fixtured in a conventional vise, and predicting how the material will behave when wall thickness varies across a single part.
Engineers often fall back on hand-welded fabrications or multi-piece assemblies, but those introduce joints, thermal distortion, and inspection headaches. A better route is to treat the geometry as a system: map the functional surfaces first, then let the manufacturing process—whether CNC contouring, metal additive, or sheet forming—dictate how the transitions between those surfaces should be blended. This shifts the conversation from “can we make this shape?” to “which process keeps the critical features stable without adding unnecessary stock or post-processing?”
The payoff shows up in reduced part count and fewer hidden failure points. A single component with a compound curvature and an internal channel can replace three or four bolted pieces, but only if the design tolerances are tied to the actual toolpath strategy rather than a generic ISO grade. Getting there requires early collaboration between design and manufacturing teams, plus a willingness to prototype in the same process that will be used for production. Without that, even the most elegant geometry stays on the screen.
FAQ
Various graphite parts used in high-temperature processes, including susceptors, wafer carriers, heating elements, crucibles, and furnace furniture. The coating conforms to complex geometries without compromising dimensional accuracy.
Silicon carbide creates an impermeable barrier that prevents particle generation and outgassing from graphite, which is critical for maintaining wafer purity. It also withstands thermal shock and resists oxidation at process temperatures.
We use chemical vapor deposition (CVD) to grow the SiC layer atom by atom. This method yields a dense, pinhole-free coating with thickness controlled within microns across the entire surface, even inside holes and edges.
Yes, our vertical CVD reactors accommodate components up to 2 meters in length. We regularly coat large PECVD trays and diffusion boats for solar manufacturers, maintaining tight flatness and minimal thermal mass increase.
Depending on the application, we apply coatings from 30 to 200 microns. For environments with aggressive chemical exposure or repeated thermal cycling, thicker coatings extend service life without sacrificing heat transfer properties.
Uncoated graphite oxidizes rapidly above 400°C, but SiC forms a protective oxide layer that slows degradation. Customers typically see three to five times longer service life, reducing downtime and replacement costs.
Yes, we strip the old coating, inspect the graphite substrate for cracks or erosion, and recoat if the part retains structural integrity. This service restores performance at a fraction of new part cost.
Each batch undergoes visual inspection under high-intensity light, thickness measurement via eddy current or microscopy, and adhesion testing per ASTM standards. We also provide certificates of conformance with lot traceability.
Conclusion
In semiconductor and solar manufacturing, the stability of graphite carriers and fixtures under aggressive thermal cycling separates functional components from production bottlenecks. A robust SiC coating does more than shield the substrate; its chemistry must hold against rapid temperature swings, thermal oxidation, and reactive process gases. The coating bonds tightly to carefully selected graphite grades that meet semiconductor-grade purity, ensuring no unwanted metallic contamination reaches the wafer surface. Uniform SiC layers across the entire carrier surface deliver repeatable performance run after run, while precise control over coating thickness allows the layer to match each furnace profile—whether a low-pressure epitaxy tool or a high-throughput diffusion furnace. For solar cell production, the demand shifts toward long-term durability under continuous thermal loading and chemical cleaning cycles, where a slightly different coating formulation and thickness strategy can extend carrier lifetime without compromising purity.
Beyond standard plates and susceptors, complex component geometries such as slotted boats, cantilever paddles, and multi-level towers require a coating approach that follows every contour without cracking or thickness variation. A manufacturer with deep experience in SiC-coated graphite understands that edge retention, hole uniformity, and corner coating integrity matter just as much as the flat surfaces. By tailoring the coating process to both the graphite grade and the final shape, production teams can achieve carriers that resist particle generation, reduce maintenance downtime, and support higher furnace throughput. This practical combination of materials science and application-specific engineering lets semiconductor fabs and solar cell producers run hotter profiles and longer campaigns with fewer carrier replacements, ultimately lowering cost per wafer while maintaining strict contamination control.
Contact Us
Contact Person: Svenja Wei
Email: [email protected]
Tel/WhatsApp: +8613567891907
Website: https://www.semicorex.com