Aluminum Parts Intake Manifold Manufacturer Best Practices for Engine Upgrades
2026-07-06
When pushing your engine to the next level, every component matters—especially the intake manifold. Finding the right aluminum parts intake manifold manufacturer can make or break your upgrade. At DDR, we’ve seen how precision-crafted manifolds unlock hidden horsepower and torque. But with so many options out there, what separates a mediocre swap from a truly transformative one? In this guide, we’ll share the best practices that set elite builders apart—from material selection to airflow dynamics—so you can avoid costly mistakes and build an engine that breathes fire.
Choosing the Right Aluminum Alloy for Intake Manifolds
Selecting the ideal aluminum alloy for an intake manifold starts with understanding the specific demands of your engine setup. For naturally aspirated street engines, affordability and ease of casting often lead builders toward 356 or A356 alloys. These contain silicon and magnesium, offering a good balance of strength, corrosion resistance, and vibration damping. The heat treatment process elevates their mechanical properties, making them suitable for moderate temperatures without going over budget. However, if your build involves forced induction or consistently elevated intake temperatures, a deeper look at high‑temperature alloys is necessary.
When boost or sustained high rpm raises under‑hood heat, creep resistance becomes a deciding factor. Alloys like 319, with higher copper content, maintain strength at temperatures where standard 356 would soften. Even more resilient options, such as 6013, bring aluminum‑silicon‑magnesium‑copper chemistry into play, delivering superb thermal stability without exotic price tags. For extreme applications—think endurance racing or ultra‑high‑boost drag engines—forged aluminum or billet‑machined pieces from 6061‑T6 provide unmatched consistency and fatigue resistance, though they demand more complex manufacturing processes. Each choice reflects a trade‑off between performance longevity and fabrication practicality.
Finally, never overlook the synergy between alloy selection and manifold design features. A stiffer material like 7075 may resist wall flex under rapid pressure changes, but its tricky weldability can complicate custom plenum or runner modifications. Meanwhile, a cast 356‑T6 component might be perfectly adequate if the manifold geometry includes generous internal radii and well‑placed ribbing. Real‑world success hinges on matching the alloy’s thermal expansion coefficient with those of the cylinder head and throttle body to maintain seal integrity. By aligning these practical considerations with power goals, you’ll land on an aluminum alloy that keeps the intake tract reliable—and the engine breathing freely—for miles and laps to come.
Advanced Casting Techniques for Improved Airflow Dynamics
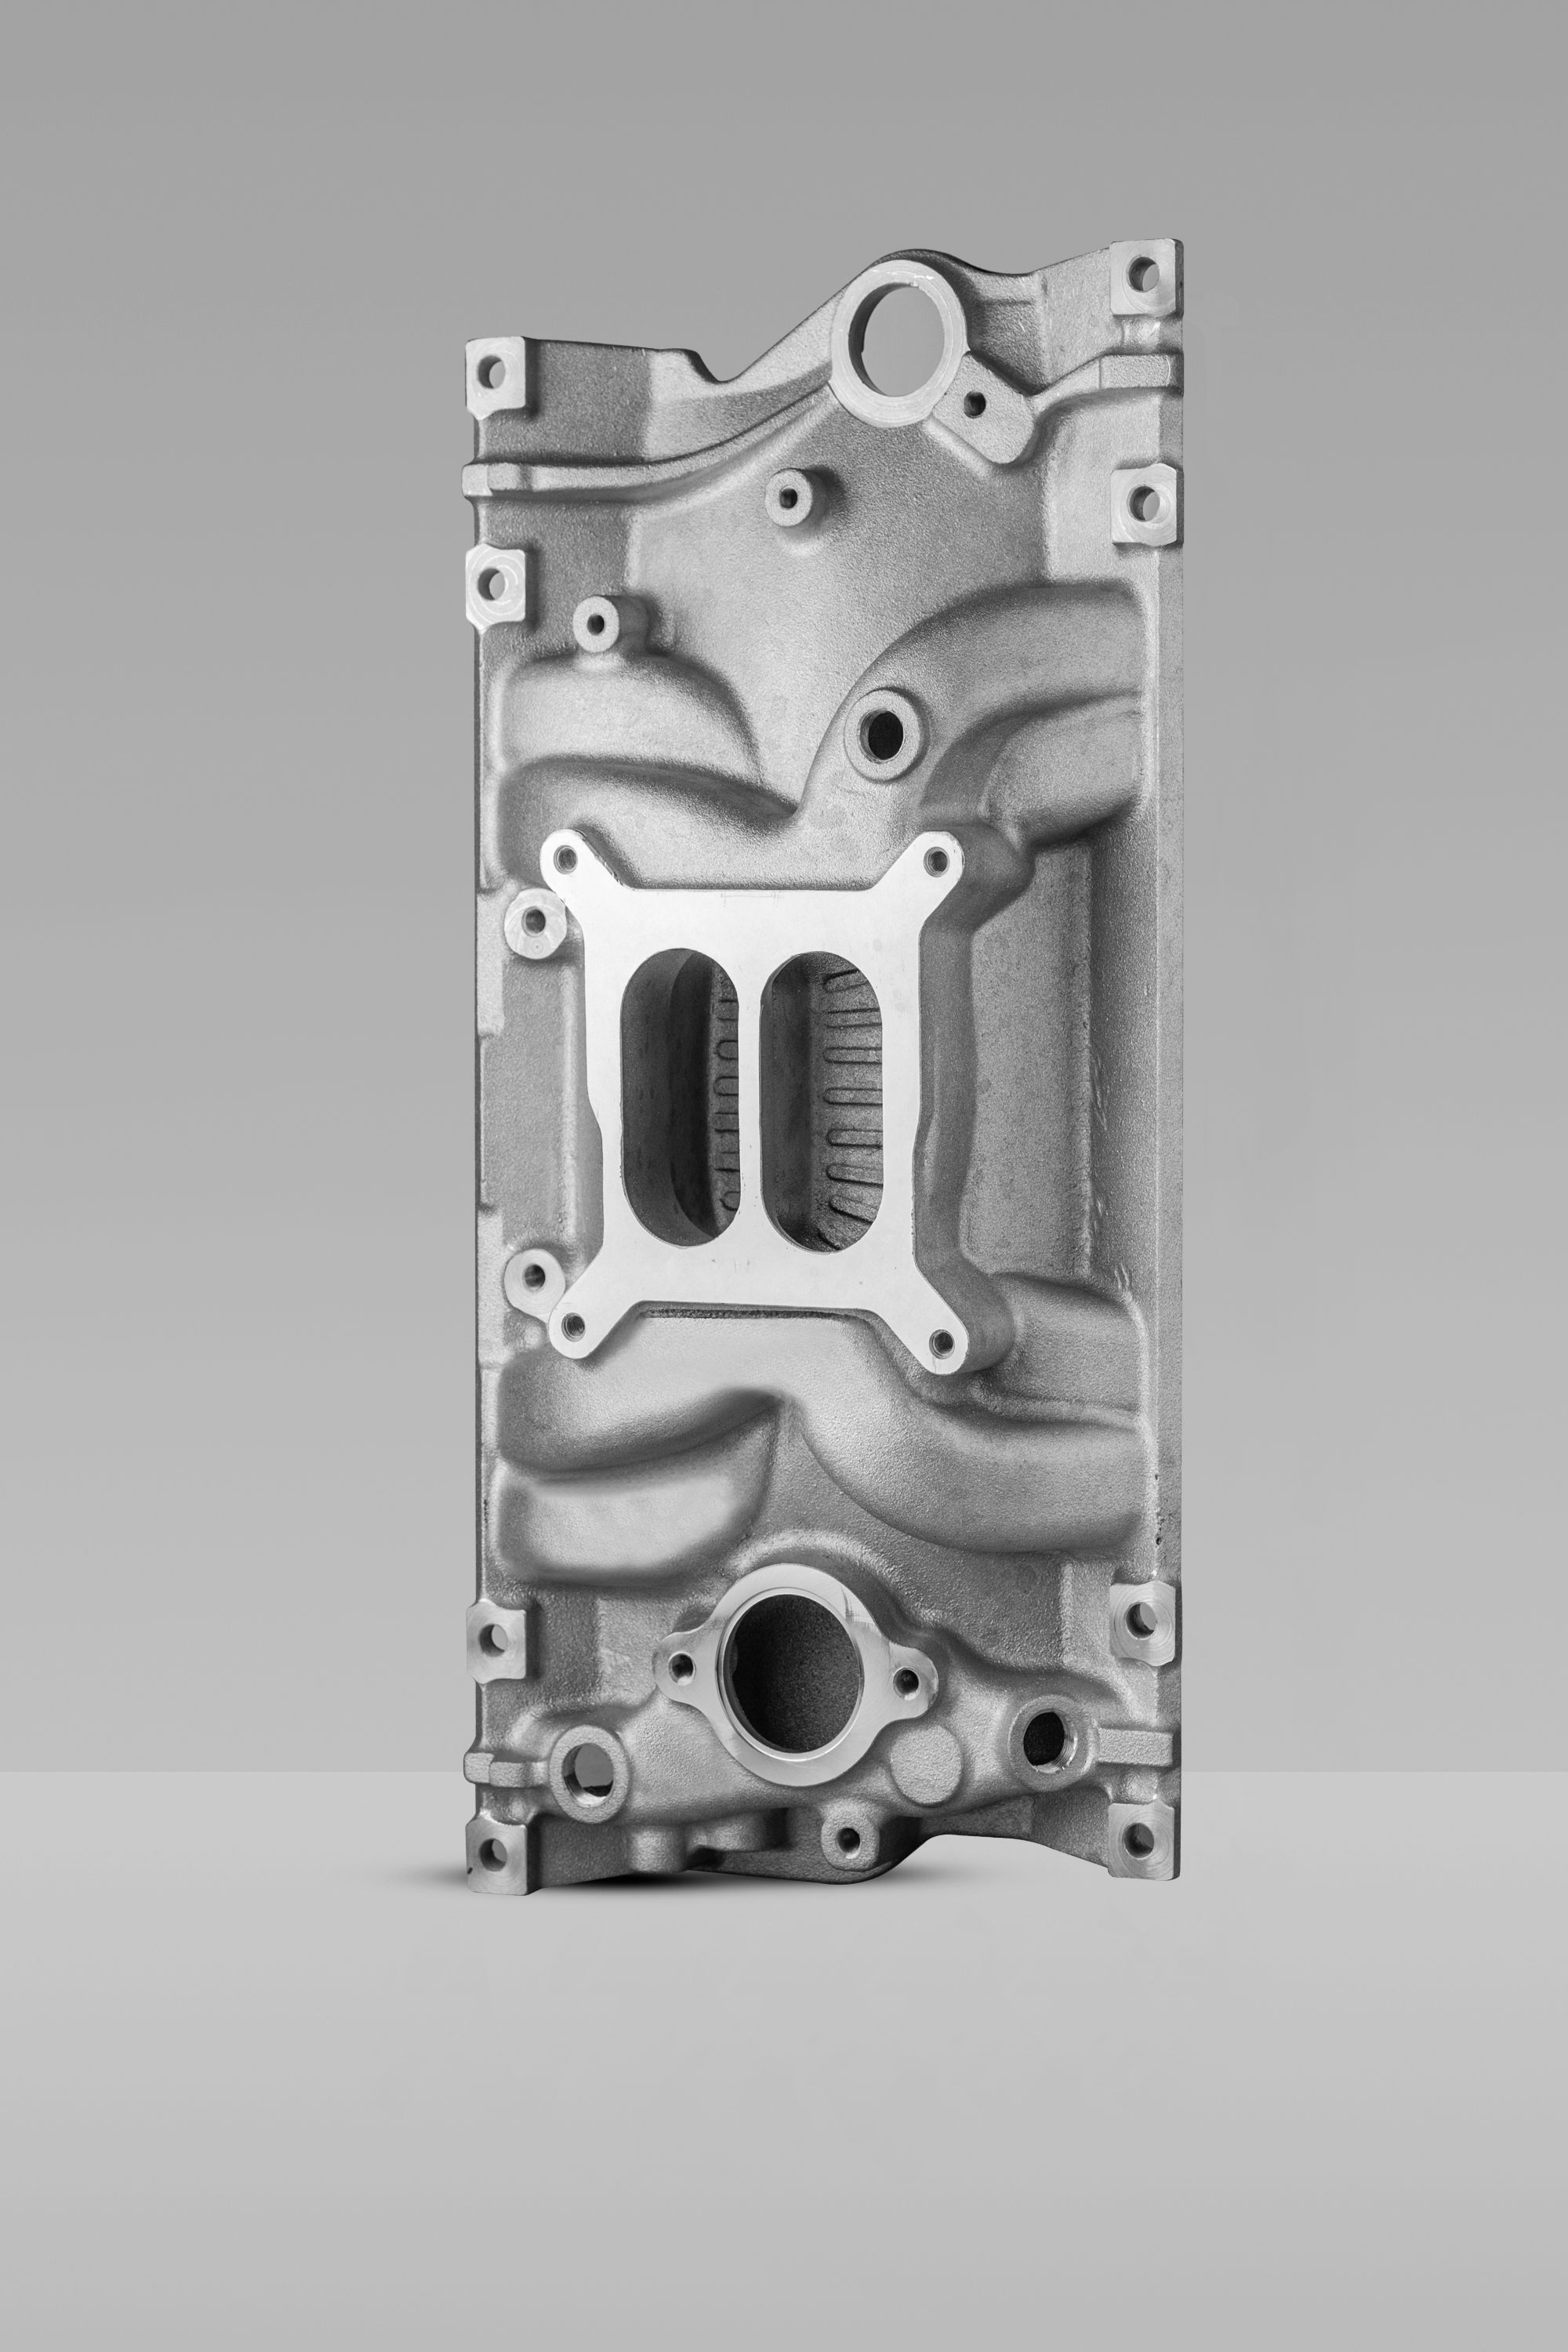
The pursuit of optimal airflow dynamics in components such as turbine blades, intake manifolds, and heat exchangers has pushed foundries beyond conventional sand casting. Minor surface irregularities or dimensional deviations can trigger turbulent flow, robbing efficiency and durability. Advanced casting processes now target these micro-level imperfections from the outset, treating the metal’s internal passageways not as an afterthought but as a critical design frontier.
Techniques like investment casting with 3D-printed wax patterns permit precisely contoured internal cores that would be impossible to achieve with traditional tooling. Vacuum casting virtually eliminates gas porosity, yielding exceptionally smooth channel walls. Meanwhile, directional solidification governs grain structure orientation to match primary flow paths, minimizing boundary layer disruption. These methods collectively ensure that the as-cast part already mirrors the aerodynamic intent, drastically reducing the need for corrective machining.
Even with these nuances, simulation-driven iterations have become indispensable. High-fidelity computational fluid dynamics (CFD) coupled with real-time X-ray process monitoring allows foundries to anticipate and correct fill-related turbulence before the first pour. The result is a tightly integrated development loop where gating systems are refined, venting is optimized, and alloy chemistry is adjusted – all in the name of delivering an internal geometry that breathes exactly as designed, free from the legacy compromises of older casting practices.
Surface Finishing Methods that Reduce Heat Soak
Controlling heat soak starts with how a surface interacts with radiant energy. Instead of relying solely on material choice, subtle alterations in texture can make a surprising difference. A finely bead-blasted or vapor-honed finish, for instance, scatters incoming light more effectively than a polished mirror surface, reducing the amount of energy that penetrates and lingers. The microscopic peaks and valleys act like a labyrinth, trapping and re-emitting heat before it has a chance to sink deep into the substrate.
Coatings designed for thermal management often carry a reputation for being thick and heavy, but modern approaches prove otherwise. Thin-film ceramic layers, barely thicker than a human hair, can fundamentally change how a part sheds heat. They work not by insulating, but by altering the surface emissivity, allowing the component to radiate warmth more freely rather than holding onto it. This shift in cooling behavior is especially useful in tight engine bays, where every degree matters and airflow is limited.
The color of a finish still matters, but not in the way many assume. While black surfaces are lauded for emissivity, the real trick is using pigments that remain stable under prolonged heat cycling. A carefully formulated matte white, for example, can sometimes outperform a cheap black paint by reflecting solar load without trapping as much thermal energy in the top layer. It’s about finding that balance between reflectivity and radiative cooling so the part stabilizes at a lower temperature, even after long runs.
Integrating Modular Designs for Future-Proof Upgrades
The core idea behind future-proof upgrades is to design each component as a self-contained module that can be swapped or enhanced without disrupting the entire system. This approach treats hardware and software as discrete building blocks, allowing new technologies to slide into place while the rest of the infrastructure remains untouched. By standardizing interfaces and communication protocols, you create a framework where updates happen in isolation, drastically reducing downtime and compatibility headaches.
Practical implementation often starts with a thorough audit of existing dependencies, mapping out which parts are most likely to evolve or become obsolete. Once those hot spots are identified, you introduce abstraction layers that decouple specific functions from the larger workflow. For example, instead of baking sensor drivers directly into the main control logic, you wrap them in a generic API so replacements require only minor configuration changes. Over time, this modular spine lets you phase in improvements piece by piece, keeping pace with innovation without the budget or logistical strain of a full-scale overhaul.
The real advantage shows itself years down the line, when new demands or market shifts would normally force a complete redesign. With a modular architecture, you simply iterate on the modules that need attention, preserving your original investment in both training and infrastructure. It's a mindset shift from building a monolithic final product to cultivating an adaptive ecosystem, one where upgrades feel like a natural evolution rather than a disruptive event.
Quality Control Processes That Ensure Perfect Fitment
Achieving a flawless fit isn't just about precise measurements during design—it demands rigorous, multi-stage checks that catch even the slightest deviations. Our quality control pipeline combines automated scanning with the trained eye of seasoned inspectors. Each component passes through coordinate-measuring machines that compare real-world dimensions against CAD models down to the micron, flagging anything that drifts beyond tolerance. Alongside these digital checks, tactile gauges and fixture-based tests simulate actual installation, ensuring that parts not only meet specs on paper but also align effortlessly in the real world.
What truly sets our process apart is the focus on real-world assembly conditions. Instead of isolating individual parts, we batch-test random samples by fitting them onto production jigs that mirror the exact mounting surfaces and adjacent components. This exposes subtle warpage, clip fatigue, or edge misalignment that solitary measurements miss. Any batch showing inconsistent engagement forces or gapping beyond 0.2mm triggers an immediate root-cause analysis and corrective action—before a single unit ships. It’s this obsession with context that turns a technically compliant piece into one that clicks home with unwavering consistency.
Beyond the factory floor, our feedback loop ties directly into design iterations. Inspection logs feed a living database that maps recurring outliers to specific tooling wear or material shifts. When patterns emerge, we refine the injection molds or adjust the stamping parameters in real time, closing the loop between detection and prevention. This proactive stance means we’re not just catching errors; we’re continuously engineering them out, maintaining a fitment standard that stays ahead of gradual drift and delivers a seamless experience, build after build.
Testing Protocols for Durability Under Boosted Conditions
Pushing components beyond their standard limits requires protocols that don’t just accelerate life but actively expose weaknesses hidden under nominal loads. Traditional steady-state testing often misses intermittent failures that emerge only when thermal and mechanical stresses compound in rapid succession. A well-designed boosted protocol layers multiple stress factors—temperature cycling, pressure surges, vibration—in overlapping sequences that mimic real-world abuse rather than isolated extremes.
Key to this approach is the use of physics-informed duty cycles, where stress levels are modulated based on actual field data, not arbitrary multipliers. We’ve found that inserting intentional soak periods at elevated conditions, followed by aggressive transients, reveals material creep and fatigue thresholds far earlier than step-stress methods. Monitoring during these protocols relies on high-fidelity sensors that capture degradation in real time, flagging subtle deviations in performance that precede catastrophic failure.
The resulting failure modes often differ from those seen in standard durability tests, requiring engineering teams to refine their root-cause investigation techniques. Post-test analysis isn’t complete without cross-sectioning and SEM imaging to validate that the boosted environment did not introduce artifacts. By correlating these findings with computational models, teams can recalibrate safety margins and confidently extend component lifetimes without overdesigning.
FAQ
It comes down to casting quality and attention to airflow dynamics. Premium manifolds often feature smoother internal surfaces, uniform wall thickness, and carefully radiused runners that minimize turbulence. Brands that invest in computational fluid dynamics testing tend to produce pieces that deliver noticeable mid-range torque gains without sacrificing top-end power.
Commonly used alloys like 356-T6 offer a solid balance of strength, weight, and heat dissipation. But some high-end makers opt for higher silicon content to improve wear resistance and thermal stability. The key is getting the heat out of the plenum quickly—well-designed cooling passages or natural heat-shedding fin designs can keep intake temperatures lower than you'd expect, especially after consecutive hard pulls.
Look for thick flanges with machined O-ring grooves instead of flat gaskets, and internally reinforced mounting bosses that resist warping under high clamping forces. Many best-in-class units also use labyrinth-style end seals and integrate dedicated sensor bungs with tapered threads that grab tighter as manifold pressure climbs, eliminating the annoying whistle-and-lean-condition issues common in forced induction setups.
Runner length directly tunes the pressure wave harmonics that cram extra air into the cylinder. A manufacturer that publishes their manifold's tuned RPM range is a sign they've done the math. For example, a long-runner design might fatten up the power band at 3,500–5,500 RPM, which pairs beautifully with a mild street cam. Shorter runners, on the other hand, shine above 6,000 RPM but can make a lumpy idle worse if the overlap period isn't matched carefully.
Beyond basic polishing, some manufacturers apply a slick ceramic-metallic coating to the plenum floor and runner walls. This isn't just for looks—it reduces surface energy so that fuel droplets bead up and re-atomize instead of forming a stagnant film. A few specialist outfits even media-blast the interior with fine glass bead to create a micro-texture that keeps the boundary layer thin without adding significant flow resistance.
The serious players don't just stick the manifold on a dyno and call it a day. They'll run back-to-back tests with multiple throttle bodies, measure cylinder-to-cylinder air distribution with a swirl meter, and sometimes even use borescope cameras to watch fuel behavior at part-throttle cruise. A few go as far as instrumenting a vehicle with pressure transducers on the road to confirm that their CFD-predicted gains hold up under actual hood heat and vibration.
It's largely about core box accuracy and how much the foundry tolerates draft angles and parting line shift. Manufacturers that invest in precision-molded cores and then CNC-machine all critical surfaces—especially at the runner entry and the port flange—deliver a product that only needs a light gasket-match at most. The frustrating alternative is a manifold where core shift leaves a step or a lip right where air velocity is highest, forcing you to grind away precious wall thickness to blend it.
At high boost, uneven distribution of air and fuel can torch a cylinder. A dual-plenum separates the plenum into two chambers with internal balancing slots, stabilizing pressure waves and giving all cylinders a fairer share. This also smooths out the erratic MAP sensor readings that a big single plenum can generate, which means cleaner tuning and less risk of detonation when you're pushing the envelope. It's an expensive trick, but for builders chasing 30+ psi, it's often the only safe bet.
Conclusion
Crafting high-performance aluminum intake manifolds starts with a deep grasp of metallurgy and airflow. The right alloy—often a heat-treatable 356 or 319 grade—is chosen not just for its strength-to-weight ratio but for its ability to resist thermal expansion during violent heat cycles. Foundries then move to low-pressure or semi-permanent mold casting, processes that yield denser parts with smoother internal walls, slashing turbulence and letting the engine gulp air more efficiently. Surface finishes like hard anodizing or thermal dispersant coatings aren't mere cosmetics; they actively fend off heat soak by reflecting engine bay radiation away from the incoming charge, preserving intake density and knock resistance. These steps turn a simple aluminum casting into a critical power enabler.
The best manufacturers think beyond the initial install. Modular intake designs with swappable plenums or adjustable runner lengths let tuners reconfigure airflow characteristics as engine setups evolve, sidestepping the need for a whole new manifold. In the inspection room, every unit faces CMM dimensional checks and leak-down tests that weed out casting shifts or pinholes before they sabotage a build. But the real proof comes from brutal dynamometer validation: prototypes endure back-to-back pulls at elevated boost pressures, heat-soaking until stable, then getting torn down for forensic checks on gasket flanges and fastener bosses. This obsessive loop of design, inspection, and torture testing ensures that when you bolt on an intake, it fits like OE, breathes like a race part, and survives whatever boost you throw at it.
Contact Us
Contact Person: Shelly
Email: [email protected]
Tel/WhatsApp: 8613967667688
Website: https://www.yongyu.com/